
What matters should be paid attention to when processing large bags of polyurethane coatings?
Many friends who want to come to discuss this topic will feel very rusty, but in specific applications, it is indeed the most frequently heard one, and it should not be easy to be rusty. Well, since the polyurethane coating processing technology is so strong, it is also so unfamiliar to people and customers. It's okay. Today, people in Henan Province can talk about a common but unfamiliar processing technology level. , Is the polyurethane coating processing technology of large bags.
1. Polyurethane coatings, not all ton bags must be polyurethane coatings. Polyurethane coatings can only be used in packaging designs that must be moisture-proof and real organisms to make them have moisture-proof and waterproof functions.
2. Polyurethane coating materials are not applicable to both pp and pe, pp is definitely not usable, only pe can be used. The bulk of polyurethane coatings that people generally see are all pe polyurethane coatings. .
3. The weight of ton bags of polyurethane coatings is not the bigger the better, nor the lighter the better. It should be distributed according to its own specific conditions.
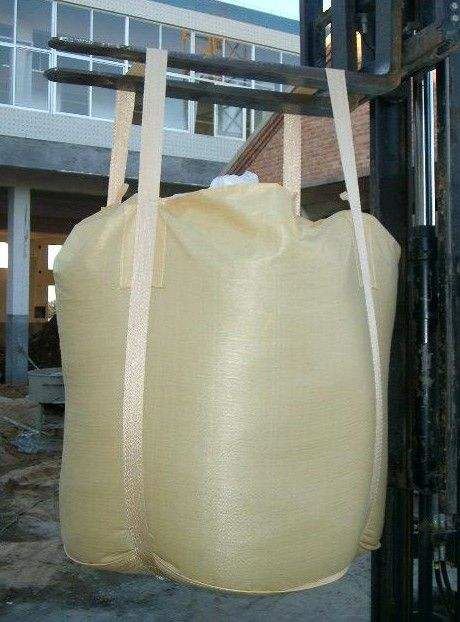
What is the root cause of the wrinkles of the ton bag at the upper traction belt roller?
Sometimes people only make large bags of goods, and there are many wrinkles on the surface. In fact, the key reason for this kind of situation is that it appears in the whole process of spinning the tube. People in Henan Province nowadays Do a detailed analysis of this problem. Under the effect of the width adjusting rod of the stent, the drum cloth is stretched into a flat tube, and the sides and surroundings of the flat tube are frictional with the width adjusting rod. If one side of the width adjustment rod is not in close contact with the tube material, under the action of the upper roller to increase the force, there is friction on both sides and the other side, which will cause the tube material on both sides and the other side to be changed within the scope of ductility. The side that does not touch the adjusting rod is long, and there is no friction or little friction in the middle position, so the tube material in the middle is not lengthened or not longer. In that way, it seems that the tube material raised by the guide roller is the same, but the tube material raised on both sides and the other side is the longer tube material without touching the expander, and the middle length becomes less. After the traction belt roller has passed, there is no driving force, and the unwinding torque has a much lower tensile force than the suction force. The tube material with longer ductility on both sides and the other side gathers more, but does not touch the width adjustment lever. The side that touches the tube material is less gathered, so that the two sides and the other side become tight edges, and the side that does not touch the width adjustment rod is loose in the middle. The amount of slack produces a convex hull according to the upper traction belt roller. When the amount of slack reaches a certain value, it will be pressed out and dismantled.